What can we help you with?
Technical flooring, delivered directly
- ESD flooring, urethane cement, terrazzo, and polished concrete
- In-house W-2 installation crews and experienced field leadership
- National service coverage with project-specific staffing plans
- Testing, documentation, and defined project closeout
- Dedicated support for corporate procurement and multi-site contracting
Phone: +1 (844) 687-1961
Electronics Manufacturing
Static dissipative and conductive ESD epoxy flooring for electronics manufacturing facilities, PCB assembly lines, SMT production areas, and EMS contract manufacturing environments. ANSI/ESD S20.20 compliant. Nationwide.
The discharge that ruins an electronics manufacturer’s quarter is the one nobody feels. A person walking an uncontrolled floor carries several thousand volts, and a transfer of under 100 volts, below human perception, can wound a MOSFET gate without killing it. The board still passes final test. It ships inside a finished product, then fails in the field months later as a warranty claim. ESD flooring for electronics manufacturing exists to close that path at the floor. Craftsman Concrete Floors installs static dissipative ESD epoxy, 1.0×10⁶ to 1.0×10⁹ Ω per ANSI/ESD STM7.1, across SMT lines, PCB assembly, wafer handling, and test and burn-in areas nationwide. Every floor ties to building steel through a conductive primer and ground straps, with testing and documentation following the methods and responsibilities in the project scope.
Electronics manufacturing flooring runs under production conditions that standard commercial epoxy never sees: solder-line foot traffic across three shifts, cart and forklift wheels, flux and solvent exposure. Standard epoxy also sits above 10¹² Ω surface resistance, well over the 10⁹ Ω dissipative ceiling, so it offers no controlled charge path at all. A poured dissipative floor is the base layer of every EPA. It covers the full production footprint. A mat protects one workstation. Pricing runs $3.34-13.55/sqft installed depending on system type, thickness, and substrate condition, informed by experience across 250+ completed projects.
Static Control on the Production Floor
An ESD Protected Area is only as continuous as its floor. Benches, wrist straps, and ionizers control fixed workstations; the floor is what qualifies the space between them, where operators, carts, and work in process move all shift. ANSI/ESD S20.20 treats the flooring-footwear system as a primary personnel grounding method, which makes the floor a qualified element of the program rather than a finish selection. The sections below map the dissipative band to the areas electronics manufacturers actually run.
SMT Lines and PCB Assembly
SMT line ESD flooring carries the highest component exposure in the plant. Feeders, pick-and-place heads, reflow load points, and manual touch-up stations put people and boards within discharge range every cycle, and PCB assembly ESD flooring extends the same controlled path through inspection, rework, and packout. The working class here is static dissipative. The band runs 1.0×10⁶ to 1.0×10⁹ Ω per STM7.1, and semiconductor ESD flooring applies the identical range with tighter verification, since die-level junction geometries fail at lower discharge energies than assembled boards. Which band a given area needs is the conductive vs dissipative question, answered on that page.
Test, Burn-In, and the Latent Defect Problem
A latent ESD defect is the failure mode that makes electronics manufacturing the most demanding ESD vertical. The wounded component still works. No inspection step catches it, and the eventual field return carries no visible damage signature to trace back to a shift or a station. Test and burn-in areas concentrate the exposure because boards are handled bare there more than anywhere else in the plant, often out of their shielding bags for hours. Closing the floor path in those rooms costs less than the diagnostic program a run of no-fault-found returns triggers.
Grounding, Verification, and the Program File
The Ground Path Is the Install
An ESD floor that reads in-band at the surface but never reaches building ground protects nothing. The performance lives in the ground path: a conductive primer or ground plane under the topcoat, copper ground straps set on the manufacturer’s spacing, and terminations tied to building steel. This is the category’s most common install failure point. Primer thinned out of spec or straps left floating produce a floor that passes a casual meter check and fails program audit. Craftsman installs the full path and documents strap locations in the closeout package.
S20.20 Qualification and Periodic Verification
The facility ESD-control program and project test plan establish the required methods, testing parties, acceptance criteria, and records. After the selected system reaches its manufacturer-approved test condition, assigned STM7.1 testing measures floor resistance. When specified, STM97.1 and STM97.2 separately evaluate the person–footwear–floor combination against the facility’s program limits. Craftsman provides the results and closeout records assigned in its executed scope; the facility sets any periodic verification plan.
Installation Around Live Production
Phased Work in Occupied Plants
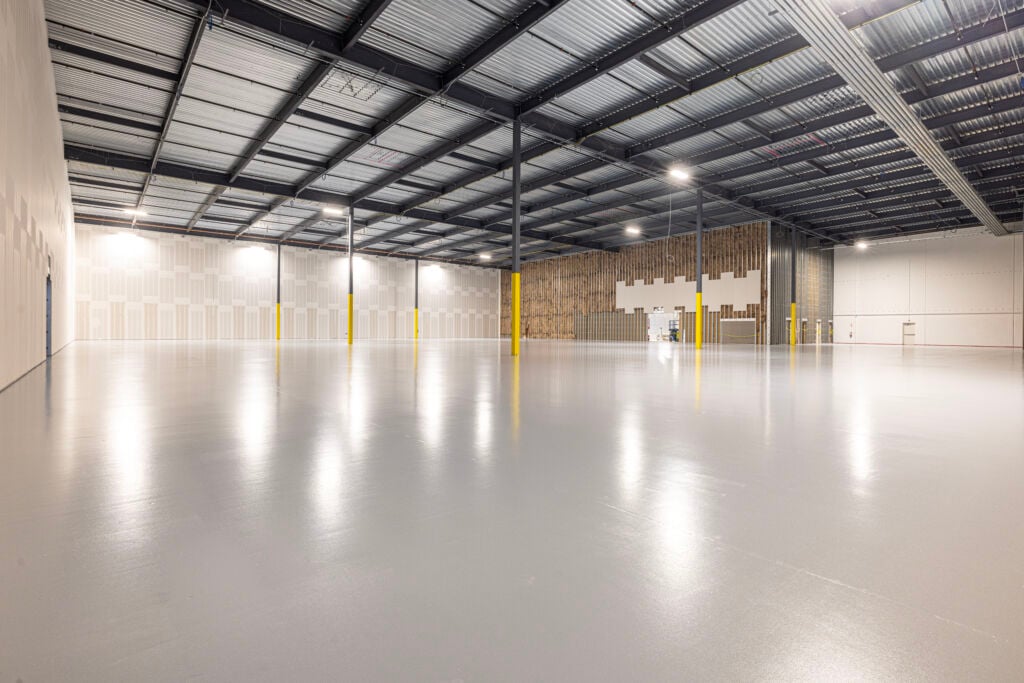
Most electronics manufacturing flooring work happens in plants that are running. Phased zone-by-zone installation can work around live operations. The selected system’s cure requirements and the project test plan determine when assigned STM7.1 floor-resistance testing occurs. Zones are sequenced against production schedules and returned to service under the agreed acceptance and handback criteria. A Dallas 34,000 sq ft Fortune 500 telecom-equipment manufacturer’s Tier-1 electronics QA facility ran exactly this way, phased through occupied space with the dissipative system verified zone by zone.
Systems and Crews
Craftsman is an Authorized SW + PIP + Sika installer. That covers the dissipative and conductive ESD epoxy families electronics plants specify — Sherwin-Williams Resuflor SCT over Resuprime ESD, PIP InhibiStat systems, and the Sikafloor 2xx ESD series. W-2 installers, not 1099 day-labor. Trained, insured, and accountable to you. In-house W-2 crews provide national service coverage, and lead time runs 1-3 weeks from contract execution, driven by material availability. Craftsman has installed industrial flooring since 1999. Electronics-manufacturing projects are performed by directly employed W-2 crews assigned companywide according to geography, system requirements, experience, availability, equipment needs, schedule, concurrent workload, facility requirements, and customer continuity. The employee roster may change by project, site, phase, and schedule; national coverage does not imply one fixed traveling crew.
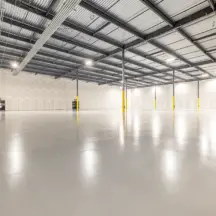
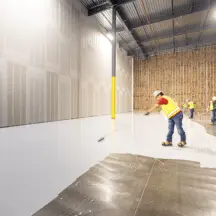
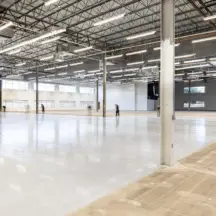
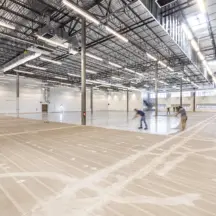
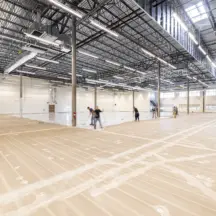
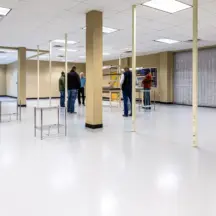
ESD Flooring Gallery
Frequently Asked Questions
$3.34-13.55/sqft installed depending on system type, thickness, and substrate condition, informed by experience across 250+ completed projects. Electronics plants typically land mid-band with a dissipative topcoat over a conductive primer, while heavy-traffic and high-build areas price higher. Large full-floor projects price below small phased retrofits per square foot.
Standard epoxy carries surface resistance above 10¹² Ω, well over the 10⁹ Ω upper bound ANSI/ESD S20.20 sets for a dissipative floor, so accumulated charge has no controlled path off a person or cart. The result is the latent defect problem. Discharges below human perception wound components that pass final test and fail in the field, and a dissipative ESD epoxy at 1.0×10⁶ to 1.0×10⁹ Ω bleeds that charge continuously to a building-steel-tied ground.
When floor-resistance testing is assigned, the installed floor is tested against project acceptance criteria after the selected system reaches its required test condition, using STM7.1. The facility’s program may separately require qualification of specified person–footwear–floor combinations using applicable STM97.1 and STM97.2 methods and program limits. The executed scope identifies who performs each test and which results and grounding records go in the facility’s ESD program file. The facility sets its periodic verification methods and schedule.
Yes. Phased zone-by-zone installation is available for running plants. Each zone reaches the selected system’s required test condition, completes the acceptance checks assigned in the project plan, and returns to service under the agreed handback criteria. The Dallas 34,000 sq ft Fortune 500 electronics QA installation was phased through occupied space.
The resistance band is usually the same. Semiconductor and cleanroom work runs the identical static dissipative 1.0×10⁶ to 1.0×10⁹ Ω with tighter verification, because die-level devices fail at lower discharge energies than assembled boards. Where a semiconductor cleanroom spec calls out materials flammability, FM 4910 governs cleanroom construction materials; it is a fire-propagation protocol, not an ESD standard, and applies only where the spec genuinely invokes it. Conductive floors below 1.0×10⁶ Ω are reserved for flammable-atmosphere and munitions work; general electronics stays in the dissipative band.
Craftsman is an Authorized SW + PIP + Sika installer. For electronics plants that means Sherwin-Williams Resuflor SCT at 15-20 mils over Resuprime ESD conductive primer, the PIP InhibiStat systems including PIP 100 ESD HB at 12-20 mils, and the Sikafloor 2xx ESD series at 24-30 mils. System selection follows the spec’s resistance band plus the area’s traffic and chemical exposure.
Nationwide. Craftsman installs electronics-manufacturing ESD flooring through directly employed W-2 crews rather than brokered or 1099 day labor. Personnel, field leadership, equipment origins, travel assumptions, and schedule are assigned companywide for the actual project according to geography, system requirements, experience, availability, equipment needs, concurrent workload, facility requirements, and customer continuity. Craftsman’s offices are service and accountability points, not fixed workforce or equipment origins.
Electronics Manufacturing ESD Flooring Knowledge Center
Related production areas and separate hazard requirements
Compliance Requirements & Testing
Systems & Selection
Project Planning & Delivery
Maintenance & Troubleshooting
Manufacturer ESD Flooring Systems
Case Studies
Craftsman Publishes 2026–2027 ESD Flooring Technical Guide
ESD Epoxy Flooring Case Study: 34,000 SF Dallas, TX